7820 Dinmore Manor - The Blog

This blog will follow the heavy overhaul of 7820 through to its return to steam. The chassis is being overhauled at Tyseley Locomotive Works whilst the boiler is being overhauled at Ian Riley's workshops.
We are working hard every weekend to bring together the hundreds of small pieces that require refurbishing to get the loco back into working order. Follow us to keep up todate with the weekly progress and who knows if you like the look of what you see you may even be tempted to join us and help put 7820 back in action.

Sunday, 2 August 2015

Saturday, 1st August 2015 - Tender Brake Gear


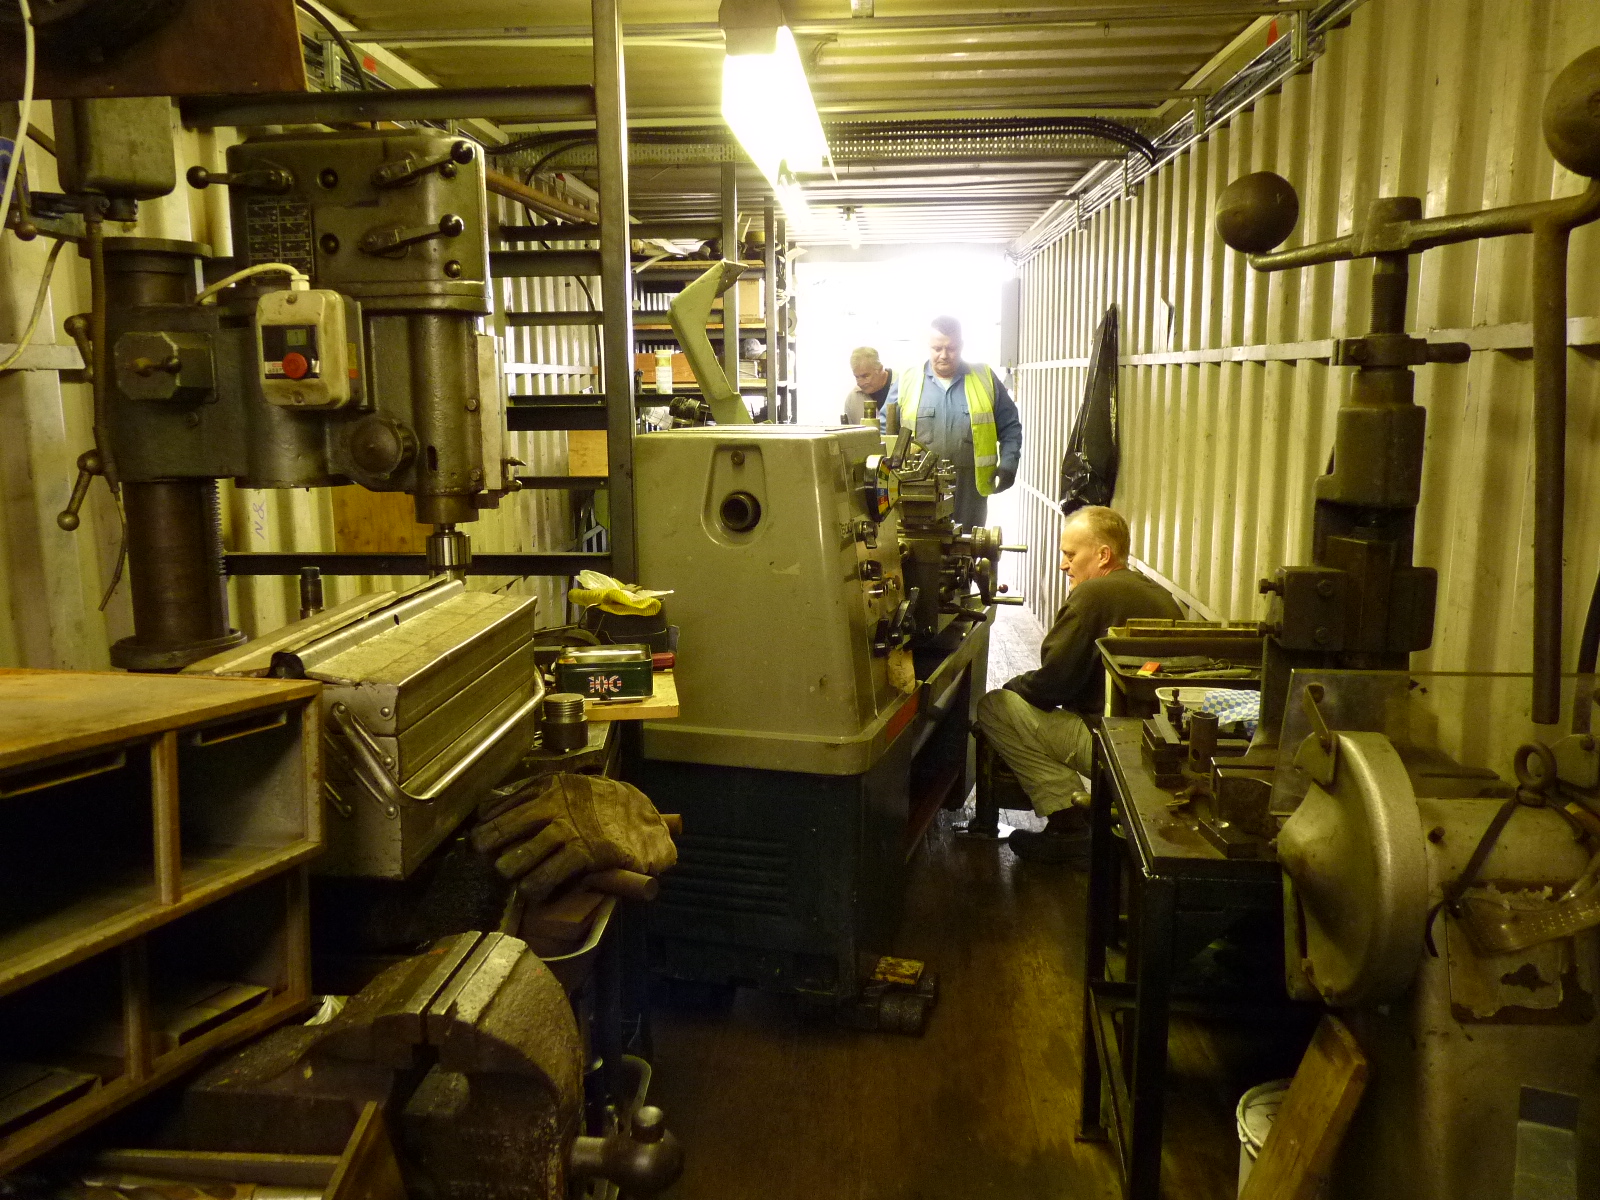
    DMLG's recently acquired lathe positioned and wired
up ready for use in the machining area

 
The turning section after reorganisation of this area


                               The Colchester Triumph 2000 lathe enters service and soon
                                shows a prodigious capacity to remove metal compared to
                                                               our previous machine


                               Not to be outdone, our other Colchester lathe is used to
                                trial a mandrel designed to assist in the machining of the
                                  outside diameter of bushes. Each bush has to be carefully
                                tailored to fit the component and, to ensure the correct interference
                                     fit is achieved, requires repeat adjustment of it's size

Wednesday, 24 June 2015

Dinmore Manor On Tour - June 2015

 
  Whilst work continues on her new tender, 7820
 has visited the Epping and Ongar Railway for their
 Gala before moving on to holiday in Paignton


                                                        7820 runs round at Ongar


                                            and enters North Weald on a service train

                                               Photographs courtesy of Paul Arnold

Tuesday, 9 June 2015

Tender Brake Gear Progress - 30.05.15

 
        Progress continues to be made on the refurbishment of
     the tender brake gear. The bearings on the end of the
  brake beams required replacement and new bushes
 have been machined to an interference fit.
          The propane torch is lit to commence heating the bush for fitting to the beam 

 
                                                   The bush is gently heated


Rotated to get an even distribution of heat

 
Finally to a red hot temperature


                                    The bush is quickly slipped onto the journal of the brake beam,
                                     the heat having expanded it to be a slide fit and the retaining
                                                 washer is placed against the bush end


                                             The retaining nut is screwed up to the washer

 
and quickly tightened to apply pressure to the bush


                                       With the retaining nut tightened, the bush will not shrink
                                     away from the thrust face washer holding this firmly in place.
                                       Six bushes have been fitted to the three brake beams and
                                      these are now complete ready for cleaning and painting.
                                       Just three more parts of the numerous parts of the brake
                                                        gear assembly are ready!

 
The brake hangers which support the brake beams
are also being re-bushed and are here seen cleaned and painted with primer
 
 Meanwhile, in a galaxy far, far away, the main brake beam
is being bushed and machined and new tender pipework is in manufacture 

Monday, 27 April 2015

Progress on the Tender

 
 With the tender frames under cover at Toddington
 work progresses on the intermediate buffer beam

 
   Plate work is renewed in readiness for assembly
 of the new drag box


  A large number of components have
     been cleaned and painted. Seen here are
   the spring hanger rocker plates and the
    new sump cover manufactured for the well tank

 
 Welding repairs have been undertaken on the
 feed cock operating handles which had suffered
from years of corrosion

 
  One of the new bushes cooling after being heat
 shrunk onto the brake beams


                           The trailing brake beam all re-bushed and ready for finish painting

Wednesday, 21 January 2015

Saturday, 17th January 2015

 
Tender Working Party
 
 
Machining of the set of 12 rubbing pads for the six
 brake hangers continues

 
         Grease nipple holes are drilled and tapped in the
lower bearing of the brake hangers

 
Another component of the brake rigging has been completely rebushed

Sunday, 4 January 2015

3rd January 2015 - Tender Progress


                                                         2015 - The Year of the Tender

                              Through the last months of 2014, progress was being made on
                               re-bushing the brake gear for the new Dinmore Manor tender.

 
      The brake hanger brackets and top bushes in the brake hangers have
     all been renewed and the lower bushes that fit to the brake beams
 are also being renewed  

 
Some progress was made on the new plate work for the new drag box


                             The tender steps were removed to facilitate cleaning and painting
                             of the frames and the 'U' shaped angle iron that carries the various
                               engine to tender pipes was trial fitted to the new frame sections

 
    In late December, the frames moved to Toddington for completion of
  the drag box and will remain there for re- erection. After removal of
     the frames, the new 3,500 gallon tank which replaces the original 4,000
 gallon Collett tender tank was placed on the jacks
 
 
    New rubbing blocks for the brake hangers have been cast and
 are being machined in readiness for fitting


                                 The brake shaft is currently 'off-site' for machining work to be
                                 completed on it and the links from this shaft to the adjusting
                                                   screws have been re-bushed

Tuesday, 7 October 2014

7th October 2014 - Tender Progress


       Whilst 'Dinmore Manor' travels far and wide in this
                    green and pleasant land, in a little corner of Gloucestershire
      that is forever Swindonian, slow but steady progress
 is being made on her 'new' tender


           Life expired piping from the tender is being sorted to act
     as patterns for new pipework. A section connecting to
 the vacuum cylinder, which is also being replaced,
 looks a little worse for wear

 
The section connecting to the reservoir cylinder
will be remanufactured


Two sections of steam heating pipe to be replaced
 

                                        On the brake shaft, the heavily corroded bearing sleeves
                                                                 have been removed


On the brake hangers, the dowel pins that hold the
pads that restrict the brake blocks movement
have been removed so that new pads can be fitted

 
One of the old pads can been seen after removal
from the brake hanger. 50 years of rust and corrosion
made them stubborn to remove
 
 
The supporting angle iron that stretches across the
  main frames and supports a host of pipes just behind
and below the drag box has been straightened and
trial fitted

 
Some of the new plate work and stiffeners for the
drag box are being trial fitted
 
TO BE CONTINUED
 

Saturday, 9 August 2014

Saturday 9th August 2014 - Midland Site


                                                   TENDER WORKING PARTY


                                         Work has continued on machining the large quantity
                                         of bushes required for the brake rigging. Work was                                       
                                         undertaken on the journals of the brake weighbar
                                        shaft to remove the heavily pitted sleeves which can
                                        be seen after removal. New sleeves will now be
                                        machined and heat shrunk onto the journals and the
                                              support bearing will be machined to suit.

Sunday, 3 August 2014

Saturday 2nd August 2014 - Midland Site


                                                     TENDER WORKING PARTY


                                          In the great Gloucestershire outback, we continue
                                          to hone our bush craft on the tender brake rigging


The new pin has been drilled for the securing split pin
 and the bracket has been re-bushed and this brake
 hanger bracket is ready for cleaning and painting
 
 
With the six brackets well on their way to completion,
attention turns to the next item, the brake hangers.
One is set up for machining to shell out the old top
bush prior to replacement 
 
 
The boring bar being set to machine the old bush
as concentric as possible to the original bore
in the bracket before chiselling out the remains of the bush

 
The top end of the hanger bracket with the bush removed


The hanger bracket is 3" wide but had been bushed
from both sides with half bushes as can be seen from
these old bushes.

Sunday, 27 July 2014

Saturday 26th July 2014 - Midlands Site


TENDER WORKING PARTY


Our gas cylinder trolley has completed is overhaul
 and is now resplendent in a coat of engine green

 
The three brake beams have been re-bushed where necessary
and friction washers added. These now require the top hat bushes
on the beam ends. Just another 12 bushes of the 70 plus 
                                              required to complete the brake rigging.

 
New pins and bushes for the brake hanger brackets
underway

 
One of the heavy components of the brake rigging
is the weigh bar shaft which fits beneath the front
end of the tender. This shaft is in particularly poor condition
requiring sleeves on both ends and new bushes and pins.
 

                                      The removal of the old bushes where the beam connects
                                      to the pull rods and adjusting screws proved to be a lengthy
                                    task as in a previous life the bushes had been welded in place.
                                    Six hours on and a few choice expletives and the four bushes
                                    finally succumbed. The faces now require the weld removing
                                              and yet more bushes and friction washers made


The new pin in place that connects the shaft to the
vacuum piston rod 

 
and a new pin for the hand brake connection. The
corroded condition of the one end journal can also be seen.
That will have to wait for another day!